
Deoxidation and degassing are two distinct steel refining processes that target different impurities in liquid steel. Deoxidation removes dissolved oxygen by adding reactive elements that bind with oxygen to form solid inclusions, while degassing removes dissolved gases, primarily hydrogen and nitrogen, by exposing steel to a reduced-pressure environment. Both processes serve clean steel production, but they address separate metallurgical problems.
Understanding the difference matters because applying the wrong treatment, or skipping one entirely, leads to different quality defects in the finished product. The sections below address the most common technical questions about how each process works, when it occurs, and which steel grades require both.
How does each process remove impurities from liquid steel?
Deoxidation removes dissolved oxygen by introducing elements with a strong chemical affinity for oxygen. These elements react with the oxygen in solution to form oxide compounds, which then separate from the steel melt as solid or liquid inclusions. Degassing, by contrast, removes dissolved gases by reducing the partial pressure of those gases above the steel bath, which drives them out of solution and into the gas phase, where they can be extracted.
In deoxidation, the reaction happens within the melt. The deoxidizing agent combines chemically with oxygen, and the resulting oxide must float out of the steel or be captured by the slag. The effectiveness of deoxidation depends on the thermodynamic stability of the oxide formed and the ability of inclusions to coagulate and rise to the surface.
In degassing, the physical principle is different. When the pressure above the steel is reduced, dissolved gases become unstable in solution and migrate to the surface as bubbles. The lower the pressure, the more completely gases are removed. This is a physical rather than a chemical reaction, which is why degassing does not consume any additive that remains in the steel.
What gases and elements does each method target?
Deoxidation targets dissolved oxygen. The most common deoxidizing agents are aluminum, silicon, and manganese, added alone or in combination. Aluminum is the most effective because it forms a very stable oxide. Silicon and manganese are weaker deoxidizers but are often used in combination or as a first-stage treatment before aluminum addition. Calcium treatment is sometimes applied afterward to modify inclusion composition and improve castability.
Degassing primarily targets hydrogen and nitrogen. Hydrogen is particularly damaging because it causes hydrogen-induced cracking, flaking, and porosity in the solidified steel. Nitrogen in excess leads to strain aging and reduced toughness in certain steel grades. Oxygen can also be partially reduced during vacuum degassing, but the process is far less efficient at oxygen removal than dedicated deoxidation with reactive agents.
It is important to note that deoxidation does not remove hydrogen or nitrogen, and degassing does not chemically bind oxygen in the way that deoxidizing agents do. The two processes are complementary rather than interchangeable.
When in the steelmaking sequence does each step occur?
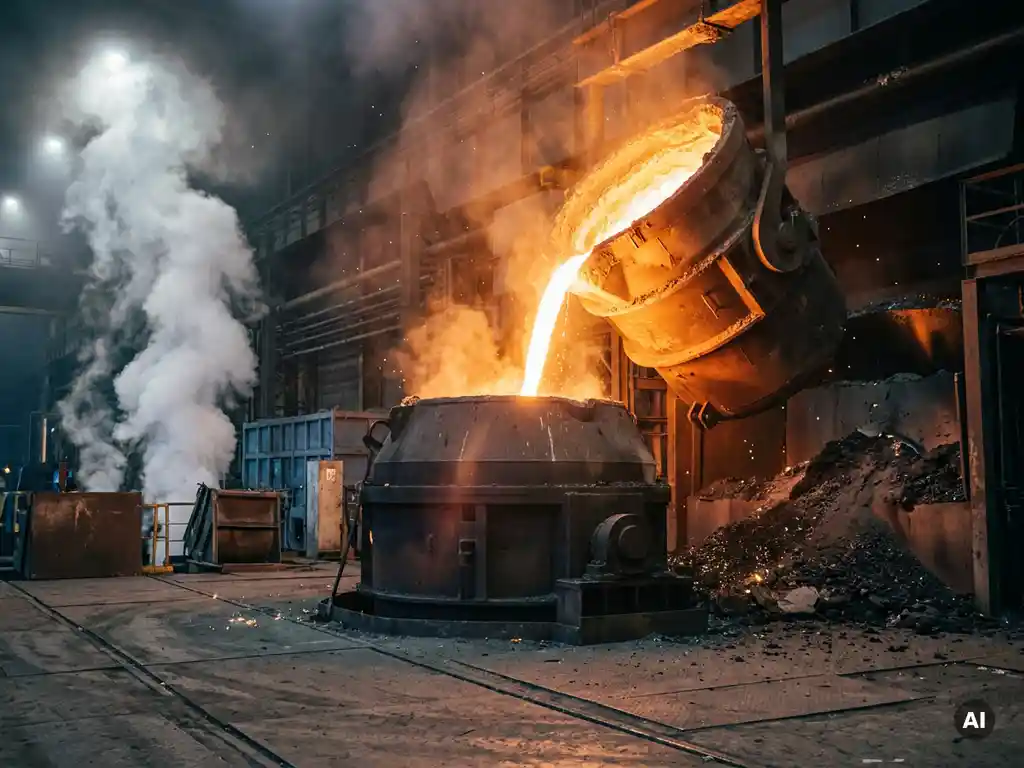
Deoxidation typically occurs immediately after tapping, when liquid steel is transferred from the converter or electric arc furnace into the ladle. At this point, oxygen content is still high from the oxidizing refining stage, and deoxidizers are added either in the tap stream or shortly after tapping is complete. This early intervention prevents excessive oxidation of alloying elements added later.
Degassing occurs later in the ladle metallurgy sequence, after primary deoxidation has already been performed. The steel must be deoxidized before vacuum treatment because high oxygen levels in the melt would make the degassing process less effective and could cause violent reactions. Degassing is therefore a secondary or tertiary step, carried out in a vacuum degassing unit before the steel proceeds to the casting stage.
In a typical sequence for high-quality steel, the order runs: tapping and primary deoxidation, ladle furnace treatment and alloying, vacuum degassing, and then casting. This sequence ensures that each refining step builds on the previous one without interfering with it.
What equipment is used for degassing versus deoxidation?
Deoxidation requires no dedicated capital equipment beyond the means to introduce the deoxidizing agents into the melt. Wire injection systems, cored wire feeders, and bulk alloy addition systems are all used to deliver aluminum, silicon, manganese, or calcium into the ladle. The process can be carried out at the ladle furnace or even during tapping at the primary furnace.
Degassing requires specialized vacuum equipment. The two most widely used systems are the RH degasser and the VD or VOD vessel. In an RH unit, steel is circulated through a vacuum vessel using a snorkel system driven by argon injection. In a VD or VOD vessel, the entire ladle is placed inside a vacuum tank and the steel surface is exposed to reduced pressure, often combined with argon stirring from the ladle bottom. Both systems require significant capital investment and are typically found in plants producing high-specification steel grades.
Ladle slide gate systems play a supporting role in the overall ladle metallurgy process. Reliable flow control at the ladle outlet is important during casting after degassing, because any uncontrolled air ingress or reoxidation at that stage can undo the quality gains achieved during refining. Systems designed to support clean steel production and reduce reoxidation are therefore directly relevant to the degassing and deoxidation sequence.
Which steel grades require both deoxidation and degassing?
Steel grades with strict limits on hydrogen, nitrogen, and oxygen all require both deoxidation and degassing. These include bearing steels, tire cord steels, high-strength low-alloy steels, tool steels, pressure vessel steels, and railway wheel and rail steels. In these applications, even small concentrations of dissolved gases or oxide inclusions can cause fatigue failure, cracking, or rejection during quality inspection.
Ultra-low-carbon steels, such as those used in automotive exposed panels, require vacuum degassing to reduce carbon content to very low levels, and deoxidation is necessary to control the resulting oxygen activity. Electrical steels and spring steels also routinely receive both treatments.
By contrast, commodity steel grades with less demanding specifications may receive deoxidation only, without vacuum degassing. The decision depends on the required mechanical properties, the intended application, and the cost of the additional processing step relative to the value of the product.
Can degassing replace deoxidation in modern steelmaking?
No, degassing cannot replace deoxidation. The two processes address fundamentally different impurities through different mechanisms, and neither can substitute for the other. Vacuum degassing reduces hydrogen and nitrogen effectively, but it does not chemically bind dissolved oxygen in the way that aluminum or silicon additions do. Without deoxidation, oxygen remains in solution and forms harmful oxide inclusions during solidification.
In practice, degassing is always preceded by at least a partial deoxidation step. If oxygen activity in the steel is too high when vacuum treatment begins, the degassing process can cause excessive foaming, slag reactions, and instability in the vacuum vessel. A controlled oxygen level before degassing is a standard process requirement, not an optional step.
Some modern steelmaking routes use degassing to assist in lowering oxygen activity indirectly, particularly through carbon-oxygen reactions at low pressure. However, this is a supplement to deoxidation practice rather than a replacement. For the vast majority of steel grades, both processes are used in sequence, with each serving a specific and irreplaceable function in the refining chain.
How KNÖLLINGER FLO-TEC supports clean steel refining
Producing clean steel depends on every step in the process chain, from deoxidation and degassing in the ladle to reliable, controlled flow at the casting stage. If reoxidation occurs at the ladle outlet during casting, it can reintroduce oxygen into the steel and form new inclusions, reducing the quality gains achieved through careful refining. Slide gate systems designed to minimize air ingress and support inert-gas shielding are therefore a relevant part of the overall clean steel strategy.
At KNÖLLINGER FLO-TEC, we develop and manufacture ladle slide gate systems specifically for steelworks that prioritize steel quality. Our systems are designed to:
- Support clean steel production by helping reduce reoxidation at the ladle outlet during casting
- Accommodate different patent-free refractory plate formats, reducing dependence on a single refractory supplier
- Provide high operational safety with reliable containment in the event of a steel leak
- Be adapted to different ladle sizes and operating requirements, including continuous casting and ingot casting applications
- Integrate with existing actuation systems where technically suitable, reducing conversion costs
If you are evaluating ladle slide gate solutions for a steelworks that produces high-specification or clean steel grades, we are ready to discuss your specific requirements. Contact our team to start a technical conversation, or explore our product range to learn more about our slide gate systems.